A manufacturing talent pipeline is not a job board with better traffic. It is a…
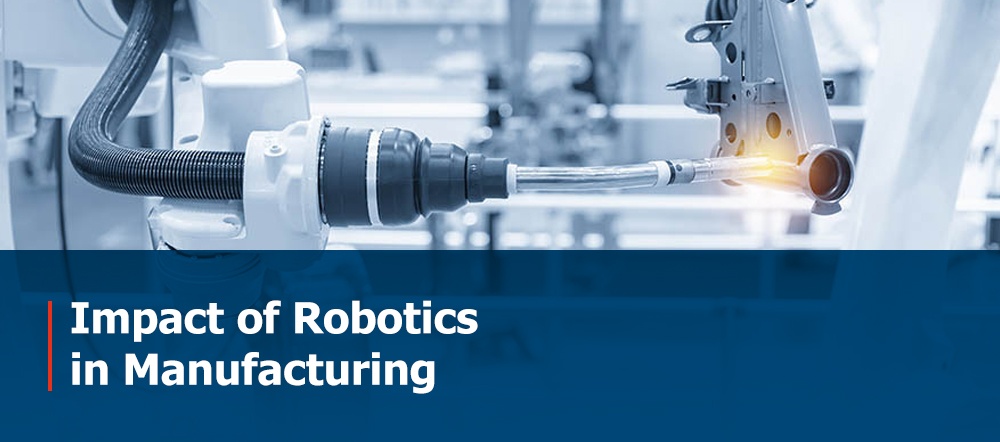
Robotics in manufacturing is no longer exclusive to large automotive plants or multinational corporations. Across South Central Pennsylvania and across the country, small and mid-sized manufacturers are adopting industrial robots and collaborative automation to compete more effectively, reduce costly errors, and redirect their workforce toward higher-value work.
This page covers what robotics in manufacturing actually means, how industrial robots work, their real benefits and genuine limitations, how the technology is evolving in 2024 and beyond, and how MANTEC helps Pennsylvania manufacturers evaluate and implement robotics without guesswork, without vendor bias, and without the kind of inflated promises that can make a robotics project fail before the first cycle runs.
What Is Robotics in Manufacturing?
Robotics in manufacturing refers to the use of programmable machines industrial robots to perform tasks in a production environment. These machines can be programmed to carry out a wide range of operations: welding, assembly, material handling, quality inspection, packaging, painting, and more.
Modern industrial robots range from large, fixed robotic arms operating within fenced safety cells to compact collaborative robots (cobots) designed to work directly alongside human employees on the open factory floor. What unites them is the ability to perform tasks with consistency, speed, and precision that are difficult to sustain at production volume with human labor alone.
The technology has existed in industrial settings since the 1960s. What has changed dramatically in recent years is the cost of entry, the flexibility of the equipment, and the sophistication of the software that makes programming and integration manageable without a team of engineers on staff. To understand how automation has reshaped U.S. manufacturing over the past two decades and what that means for small and mid-size manufacturers todaysee our in-depth industry analysis.
How Industrial Robots Work in Manufacturing
Robotic Arms and Automated Assembly
The most common type of industrial robot is the articulated robotic arm a multi-jointed machine that mimics the range of motion of a human arm, but with more joints, higher repeatability, and unlimited endurance. These arms are programmed with specific movements and toolpaths and can be reprogrammed as production requirements change. Robotic arms are widely deployed for welding, fastening, adhesive application, material placement, and machine tending.
Collaborative Robots (Cobots) on the Factory Floor
Collaborative robots (cobots) are designed to operate safely in close proximity to human workers without the traditional physical barriers that enclose conventional industrial robots. They use force-limiting sensors, camera systems, and speed restrictions to prevent injury. Cobots are generally easier to program, more flexible across different tasks, and available at a lower price point than conventional industrial robots making them a practical entry point for smaller manufacturers.
The trade-off is speed and payload capacity. Cobots are well-suited for light assembly, inspection, and pick-and-place tasks where human-robot collaboration is genuinely valuable. For high-speed, high-force applications welding, stamping, heavy material handling conventional industrial robots remain more capable.
Machine Vision and Sensing Technology
Modern robots increasingly combine motion control with machine vision camera systems and AI-powered software and that allow the robot to see and interpret its environment. Vision-guided robots can identify parts regardless of their exact orientation in a bin, detect surface defects in real time during a quality inspection cycle, or adjust their toolpath based on part variation. This capability has dramatically expanded the range of tasks that robots can handle without requiring perfectly controlled inputs.
Key Applications of Robots in Manufacturing
Most industrial robots are deployed to handle tasks that are repetitive, physically demanding, hazardous, or require a level of precision that human workers struggle to maintain consistently at volume. When workers are freed from these tasks, they can redirect their attention to roles that require judgment, problem-solving, and skilled decision-making.
A study from the market research company Vanson Bourne revealed 23% of unplanned downtime in the manufacturing sector occurs because of human error. This number is especially illuminating when compared to 9% of downtime in other industries. Manufacturing suffers more than most fields when it comes to human mistakes, as it’s not uncommon for one issue to slow down or stop an entire assembly line.
That is only one reason why the future of robotics in manufacturing is looking bright. For this sector, the projected demand for advanced robotics is expected to rise to $3.7 billion by 2021. This number encompasses a worldwide scale, meaning business professionals and production managers across the globe recognize the value of industrial robots. These skilled machines are evolving in ways many people could’ve only dreamed of, but like all things, they come with pros and cons.
For manufacturing executives and operations leaders ready to go beyond robotics into AI-powered production, MANTEC’s AI for Manufacturing Leaders course delivers a focused half-day session covering applied AI strategies for the shop floor.
Modern robotics systems generate rich streams of real-time production data. Learn how to leverage big data to improve manufacturing operations and turn that sensor data into continuous process improvements.
Welding and Assembly Automation
Welding is one of the most established applications for industrial robots. Robotic welding systems deliver consistent weld quality at speeds and volumes that human welders cannot sustain, while eliminating worker exposure to UV radiation, fumes, and extreme heat. Robotic assembly fastening, adhesive application, press-fitting follows the same logic: high-volume, repetitive work done consistently with minimal variation.
Material Handling and Pick-and-Place
Robots move materials, components, and finished products between stations, into packaging, or onto pallets far faster and more consistently than manual labor. Pick-and-place operations reduce per-unit handling time, minimize ergonomic strain injuries among workers, and maintain a predictable, measurable pace of production all of which contribute to more reliable throughput.
Quality Inspection and Machine Vision
Integrating machine vision systems into the production line allows robots to perform 100% inspection at full production speed something manual sampling cannot achieve. Vision-based inspection detects surface defects, dimensional variation, assembly errors, and missing components that human inspectors may miss during extended production runs. Moving inspection inline eliminates the bottleneck of offline quality checks and enables real-time feedback to the process.
Lights-Out Manufacturing
Lights-out manufacturing is the operation of a production facility with no human presence during production — machines run autonomously around the clock, without lights, climate control, or shift changeovers. It represents the most aggressive form of automation and is genuinely achievable for manufacturers with well-defined, highly standardized production processes and sufficient volume to justify the capital investment.
Benefits of Industrial Robots in Manufacturing
Higher Output and Consistent Cycle Times
Industrial robots operate continuously without fatigue, breaks, or shift changes. A robot running on a night shift produces the same output as one running at 9 a.m. on Monday — with no variation in speed or accuracy. For manufacturers running multiple shifts to meet demand, this consistency translates directly into higher throughput and more predictable production scheduling.
Unplanned downtime caused by human error is also a significant production cost. Research from the manufacturing sector consistently identifies human error as a leading cause of unplanned stoppages — one frequently cited figure is approximately 23% of unplanned manufacturing downtime attributable to human error, more than double the rate seen in other industries. Robotics reduces that exposure on the tasks they handle.
Lower Long-Term Operating Costs
The upfront investment in robotics can be significant, and the full financial picture — including integration, programming, maintenance, and training — needs honest evaluation before a commitment is made. That said, the long-term cost case for well-matched applications is typically compelling. Reduced scrap rates, lower rework costs, fewer injury-related absences, and more predictable labor requirements all contribute to a return on investment that typically emerges fully within 2–4 years for volume applications.
MANTEC’s interactive robotics ROI calculator at /robotics-on-the-line-simple-roi-calculator-adoption-roadmap/ is designed specifically to help Pennsylvania manufacturers model the financial case for their specific operation — using their own cycle times, error rates, and labor costs, not industry averages.
Improved Worker Safety
Removing workers from physically demanding, repetitive, or hazardous tasks is one of the most underweighted arguments for robotics adoption. Ergonomic injuries, repetitive motion disorders, burns, exposure to chemicals and fumes, and strain from heavy lifting represent significant workers’ compensation costs, productivity losses, and human costs that don’t always appear on the initial business case spreadsheet. Robots handling these tasks reduce that risk directly.
Greater Precision and Product Consistency
Industrial robots apply the same force, the same speed, and the same toolpath on the ten-thousandth cycle as on the first. Holding that level of consistency across extended production runs — especially for precision components, tight tolerances, or high-value assemblies — is genuinely difficult with human operators working repetitive tasks. The result is fewer defects, lower scrap rates, and a more reliable end product.
Pros & Cons of Robots in Manufacturing
An honest evaluation of robotics requires giving the concerns the same weight as the benefits. Here is a balanced summary:
Advantages:
- Significant ROI potential over the life of the equipment on well-matched applications
- Reduced long-term operating costs through lower scrap, rework, and injury rates
- Improved product quality and dimensional consistency
- Enhanced worker safety in hazardous or ergonomically demanding roles
- Greater throughput capacity without proportional increases in labor cost
- 24/7 production capability without shift premiums or attendance risk
Considerations and Risks:
- High upfront capital cost and integration expense full project cost is typically higher than equipment price alone
- Integration complexity in legacy production environments with inconsistent inputs or variable processes
- Workforce training requirements and change management demands that are often underestimated
- Cybersecurity vulnerabilities in IoT-connected robotic systems
- Limited flexibility for highly variable products, low-volume runs, or processes that change frequently
- Maintenance requirements and dependency on specialized support for repairs and reprogramming
Understanding these trade-offs accurately and matching the technology to the right application is where experienced independent guidance makes a real difference. MANTEC provides that guidance without vendor affiliation.
How Robotics Technology Is Evolving
The history of robots in manufacturing is expansive. Through the last few decades, these machines have steadily increased in their number of applications and efficiency. Though many see them as modern marvels, robotic manufacturing systems have been around for much longer. The inventor George Devol filed a patent for the first industrial robot in 1954, and the prototype came to life in 1961. It looked and functioned much like today’s robotic arms, able to carry 500 pounds and pull off tasks once thought exclusive to humans.
From there, these machine-based arms became a familiar sight in automotive factories and other manufacturing plants. Now, robots come with numerous features and capabilities that make them more unique, flexible and productive than before. Collaborative robots, or cobots, can work on the factory floor alongside humans for a faster, more efficient workflow. Many can even accommodate physical interaction, such as a worker physically adjusting the machine’s movements so it can memorize and repeat those steps on its own.
Both within and outside of the manufacturing field, robots are gaining senses such as touch and vision. These innovations make a major difference in a robot’s capabilities, allowing it to accomplish feats it couldn’t have done otherwise:
- Touch: Some recycling facilities employ robots that can identify and separate waste depending on the texture. Combining this feature with vision-based machine learning makes robots far more adept at sorting refuse than human workers, which can relieve them of the dangerous work of waste management. MIT recently created a machine that can predict what object or part of an item it is touching from tactile input alone.
- Sight: Some robots contain Light Detection and Ranging (LiDAR) sensors, which allow them to judge distances by using laser reflections. This sense is comparable to echolocation in animals like bats and dolphins — sound waves help these creatures pinpoint an object’s location. A notable example comes from FedEx’s SameDay Bots, which can navigate around people and objects using LiDAR.
- Hearing: Much like LiDAR technology and echolocation, some robots can use a form of technology called laser vibrometry to detect vibrations. This ability essentially allows them to hear basic sounds and even conversations. Although this is currently more common in consumer electronics like smart devices it may soon make its way to manufacturing robotics as well.
Industrial IoT and Connected Manufacturing
The Industrial Internet of Things (IIoT) connects robotic systems to cloud-based platforms and other production equipment, enabling real-time monitoring, data collection, and automated decision-making across the factory floor. A robot equipped with IIoT sensors can report its own performance metrics, signal approaching maintenance needs before a failure occurs, and share data with other machines and systems across the production network enabling the kind of predictive analytics and coordinated scheduling that previously required dedicated teams.
AI and Machine Learning in Industrial Robots
Artificial intelligence is expanding the range of tasks that industrial robots can handle independently. Rather than following a fixed, pre-programmed sequence, AI-enabled robots can adapt their behavior based on visual input, sensor data, and learned patterns from previous cycles. This capability is particularly significant for applications like quality inspection, bin picking, and part identification tasks involving enough variability that conventional programming approaches struggle to handle them reliably.
Human-Robot Collaboration and Cobot Advances
The trajectory of collaborative robotics is toward greater intelligence, lower cost, and broader applicability. Declining hardware costs, simpler programming interfaces, and improving force and vision sensing are making cobots practical in environments that could not have justified the investment five years ago. Rather than replacing workers on the factory floor, the most productive implementations tend to involve humans and robots working in structured collaboration humans providing judgment, adaptability, and skilled decision-making; robots providing speed, precision, and endurance.
Cybersecurity in Connected Manufacturing
As more robotic systems connect to networks and cloud platforms, their cybersecurity exposure grows. Manufacturing operations that integrate IoT-connected robotics need to address security at multiple levels: the robot’s own firmware, the integration layer between robots and production systems, and the broader operational network. This is not a theoretical risk cyberattacks targeting connected manufacturing equipment are increasing, and the consequences of a compromised robotic system can halt production entirely. MANTEC supports manufacturers with technology planning that includes cybersecurity readiness as part of any broader automation or connectivity initiative. See also: MANTEC’s CMMC compliance support for defense contractors with connected manufacturing systems.
The Future of Robotics in Manufacturing
Several developments are shaping the next generation of industrial robotics:
- Cobots becoming more accessible. Falling hardware costs, better safety sensing, and simpler programming tools are making collaborative robots practical for manufacturers with 50–200 employees who previously couldn’t justify the investment.
- AI-driven adaptability. Future robots will handle significantly greater variability in their environments, reducing the need for perfectly controlled inputs and enabling deployment in more complex, less structured production scenarios.
- Tighter ERP and MES integration. For manufacturers looking to connect robotics and automation systems with their enterprise resource planning platform, MANTEC’s ERP consulting services ensure seamless data flow and reporting across your entire operation.
- Continued cost reduction. The ROI calculation for robotics adoption continues to improve as hardware costs fall and integration tooling matures. Applications that weren’t financially viable at 2020 prices are crossing the payback threshold now.
Integrating Robotics Into Your Manufacturing Operation
The gap between “considering robotics” and “running robotics successfully” is real — and it is where manufacturers encounter unexpected costs, delays, and disappointing results. A structured, evidence-based approach is the difference between a successful installation and a machine that sits idle.
Assessing Technology Readiness
Before committing capital, manufacturers need honest answers to a short list of critical questions: Is the process standardized enough to be automated without constant reprogramming? Is production volume sufficient to justify the investment? Is the facility infrastructure power, floor space, safety barriers, ventilation ready to support the equipment? What is the current process quality, and will it improve or stay the same with automation? MANTEC’s technology advisers work through these questions with manufacturers before a vendor is ever contacted.
Building the Business Case
A credible financial case requires real data: current cycle times, error rates, rework costs, labor expense per unit, injury frequency and cost, and projected throughput requirements. MANTEC’s robotics ROI calculator is a practical starting point for modeling the financial picture using your specific numbers not industry benchmarks that may not reflect your operation.
Supporting Your Workforce Through the Transition
Workforce planning is consistently the most underinvested aspect of robotics adoption. Employees need to understand clearly how their roles will change, what new skills will be required, and how the organization will support them through the transition. When this is managed poorly, the result is resistance, turnover, and a workforce that doesn’t maintain the equipment or processes it depends on. MANTEC’s workforce engagement services address this directly helping manufacturers communicate change effectively and develop the internal capabilities needed to operate and sustain new technology.
How MANTEC Helps Pennsylvania Manufacturers Implement Robotics
MANTEC is South Central Pennsylvania’s Manufacturing Extension Partnership (MEP) center, providing hands-on consulting to small and mid-sized manufacturers across York, Lancaster, Cumberland, Dauphin, Adams, Franklin, Fulton, Lebanon, and Perry counties. We are part of the MEP National Network a public-private partnership funded through NIST that supports U.S. manufacturers with independent, practical guidance.
MANTEC’s manufacturing technology services team can conduct a facility assessment and help you identify the right robotics and automation solutions for your production environment and budget.
Our approach to robotics and manufacturing technology is not theoretical, and we are not affiliated with any robotics vendor or integrator. When a manufacturer comes to us with interest in automation, we start with their specific production environment:
- Technology readiness assessment : identifying which processes are genuine candidates for automation and which aren’t ready yet, so capital isn’t committed to the wrong application
- Vendor and integrator evaluation support : helping manufacturers navigate the market, ask the right questions, and make informed decisions without being sold to
- ROI modeling and financial justification : developing the business case needed to move a proposal through ownership or leadership
- Implementation oversight : keeping the project aligned with production goals during installation and commissioning
- Workforce development : preparing operators, maintenance technicians, and supervisors for the changes that come with new technology
If you are a small or mid-sized manufacturer in South Central Pennsylvania exploring whether robotics makes sense for your operation, the right first step is a conversation not a purchasing decision. Contact a MANTEC technology adviser through our website or call 717-843-5054.
Frequently Asked Questions About Robotics in Manufacturing
Q1: What types of robots are most commonly used in manufacturing?
A: The most common types include articulated robotic arms (used for welding, assembly, and material handling), SCARA robots (high-speed pick-and-place operations), delta robots (packaging and sorting), and collaborative robots (cobots) designed to work alongside human workers. The right type depends on the task, production volume, space constraints, and required cycle time. MANTEC can help you evaluate which type is the right fit for your specific application.
Q2: How much does it cost to implement industrial robots?
A: Costs vary widely depending on robot type, application complexity, facility preparation requirements, and integration work. A basic cobot installation can start around $25,000–$50,000; a fully integrated robotic welding cell or complex assembly installation can exceed $250,000. Total cost of ownership including programming, maintenance, spare parts, and training is as important to evaluate as the purchase price. Use MANTEC’s robotics ROI calculator to model the financial case for your specific scenario using your real numbers.
Q3: Will robots replace manufacturing workers?
A: In most smaller manufacturing environments, the realistic outcome is job transformation rather than wholesale replacement. Robots take over repetitive, dangerous, or precision-demanding tasks; workers move into roles involving programming oversight, maintenance, quality management, and process improvement. The transition requires planning, training, and clear communication with the workforce all of which MANTEC’s workforce services support directly.
Q4: What is the typical ROI timeline for industrial robots?
A: For well-matched, high-volume applications, most manufacturers see full payback within 2–4 years. Applications with multiple shifts, high rework rates, or significant injury-related labor costs tend to see faster payback periods. Operations with low-volume, high-variability production may see much longer payback which is why accurate modeling using real data from your operation matters more than industry averages.
Q5: What is a cobot and how is it different from an industrial robot?
A: A collaborative robot (cobot) is designed to operate safely in close proximity to human workers typically without safety fencing using force-limiting sensors, speed restrictions, and vision-based safety systems. Traditional industrial robots operate at higher speeds and forces and require physical barriers to protect nearby workers. Cobots are easier to program and more flexible across different tasks, but sacrifice speed and payload capacity. Cobots are generally the better choice for light assembly, inspection, and human-robot collaboration scenarios; conventional industrial robots are better suited for high-speed, high-force, or high-volume applications.
Q6: How do I know if my manufacturing process is a good candidate for automation?
A: The strongest candidates share several characteristics: high production volumes of a standardized part or product, tasks that are repetitive, physically demanding, or prone to human error, and processes where consistent cycle time directly affects output. If your process changes frequently, involves significant product variability, or runs at low volume, robotics may not be the right fit at this time. A MANTEC technology adviser can help you assess your specific processes honestly before capital is committed.
Q7: Does MANTEC help with robotics vendor selection?
A: Yes. MANTEC provides independent, vendor-neutral guidance on technology selection. We are not affiliated with any robotics manufacturer or integrator, which means our recommendations are based entirely on your requirements and production goals not a sales relationship. We help manufacturers evaluate options, ask the right questions during vendor conversations, and make informed decisions without responding to sales pressure alone.
Ready to Explore Robotics for Your Pennsylvania Manufacturing Operation?
MANTEC has helped manufacturers across York, Lancaster, Cumberland, Dauphin, and surrounding counties evaluate and adopt manufacturing technology at every stage from first-time exploration to specific implementation challenges. Whether you are thinking about robotics for the first time or troubleshooting an existing automation project, we are here to help.
See real-world results from Pennsylvania manufacturers who have worked with MANTEC to modernize operations through technology adoption, process improvement, and workforce development.
Contact a MANTEC technology adviser or call us directly at 717-843-5054.
Related Posts